Monday, April 2, 2012
Datsun/Nissan 1969-74 Drive Axles Repair Manual
1969-74 DATSUN SEPARATE CARRIER
MODELS COVERED:- B210 (1974)
- 311 (1968-70)
- 510 Station Wagon (1968-72)
- 521 Pickup (1969-72)
- 610 Station Wagon (1973-74)
- 620 Pickup (1972-74)
- 710 (1974)
- 1200 (1971-73)
DESCRIPTION
Differential gear carrier assembly has a hypoid type pinion and ring gear set. The gear carrier is constructed of cast iron. The drive pinion is mounted in two tapered roller bearings that are preloaded by a collapsible spacer or by non-adjustable spacer. Drive pinion is aligned into position with a shim located between shoulder on drive pinion and rear bearing. Differential case is supported in carrier by two tapered roller side bearings. The side bearings are preloaded by inserting shims between bearings and differential. Case housed two side bears that mesh with two pinion gears mounted on a pinion shaft. The pinion shaft is held in case with a lock pin. Pinions and side gears are set in front of thrust washers.
AXLE RATIO AND IDENTIFICATION
Datsun does not identify rear axle with a particular outside identification marking. However all models are some basic type of removable carrier rear axle. It should be noted that part or model numbers may vary between vehicle models, but the internal design is similar. The following table indicates the axle ratios that are available, any not found in table may be computed by dividing number of ring gear teeth by number of pinion gear teeth.
Rear Axle Ratio
Application Ratio
B210
1974............................... 3.900
610
1973................................3.889
620
1972-74.
Man. Trans................4.375
Auto. Trans...............4.625
710
1974
Man. Trans................4.111
Auto. Trans...............3.889
1200
1971-73..........................3.900
REMOVAL AND INSTALLATION
AXLE SHAFT AND BEARINGS
Removal 311, 521 and 620 - Raise vehicle and place an safety stands, remove rear wheels. Disconnect and plug wheel cylinder inlet line, remove brake drum. If drum is hard to pull off, lightly tap outside of casting to free or back off shoe adjuster(s). Remove four brake assembly retaining nuts. Pull out axle shaft and brake assembly using slide hammer.
Inspection - Using a dial indicator, check axle shaft deflection, maximum allowable bending is .039" (1.0 mm). Replace axle shaft or components if any of the following conditions exist seal surface and/or thrust block side end surface scared; bearing rust, rough rolling or chipped; oil seal cracked or otherwisde damaged.
Disassembly - Place axle in suitable work stand and bend lock washer tabs away from nut. Remove lock nut, then using axle shaft bearing puller, withdraw wheel bearing with cage and brake assembly. If necessary, remove oil seal from inside bearing cage. With a brass drift and hammer top against bearing race surface until race is removed.
Reassembly - Fit bearing race and rubber grease seal to cage by carefully seating with brass hammer. After seal installation, fill up with grease. Install brake assembly and bearing cage on axle, then fit bearing race using a brass drift. Press in new bearing then tighten lock nut and bend up lock tabs.


 |
| REMOVING LOCK NUT (620 MODEL SHOWN) |
Removal B210, 510, 610, 710 and 1200 - Raise rear of vehicle and support on safety stands, remove rear wheels. Disconnect wheel cylinder inlet line and plug opening. Disconnect parkign brake linkage and move out-of-way. Remove brake drum and four nuts mounting brake book plate to axle case. Using suitable puller, remove axle shaft assembly. Remove oil seal and replace at this time.
 |
| CLEARANCE BETWEEN WHEEL BEARING AND AXLE TUBE |
Disassembly - Place axle shaft assembly into suitable holding device and chisel off wheel bearing collar; then remove wheel bearing.
Reassembly - Install bearing spacer, bearing and new bearing collar onto axle shaft. Bearing collar must be installed under 3-5 tons foce.
Installation - Fit axle shaft into axle housing being careful not to damage oil seal. Adjust clearance between wheel bearing and axle tube and using .039" (1.0 mm) shim as shown in illustration. Measure axial end play with a dial indicator, reading should be .018" (.45 mm). Reverse removal procedure for remaining components
PINION FLANGE SEAL
NOTE - The following procdure can only be performed on those models that use non-adjustable spacer (not collapsible spacer type).
Removal - Raise and support rear end of vehicle, then drain gear oil. Index mark propeller shaft and companion flange, then detach shaft and wire out-of-way. Remove drive pinion nut and using suitable puller extract companion flange. With special tool (ST33290001) remove oil seal.
Installation - Set new oil seal into position and pack grease between seal lips. Position companion flange and flat washer on drive pinion, then tighten nut and check bearing preload.
DIFFERENTIAL CARRIER
Removal - Raise and support vehicle on safety stands placed under rear axle housing. Drain gear lubricatn. Index mark propeller shaft and remove. Withdraw rear axle shafts as previously described. Remove nuts mounting differential gear carrier to axle housing and lift out gear carrier.
Installation - To install differential gear carrier, reverse removal procedure and tighten nuts.
AXLE ASSEMBLY
Removal - Raise rear of vehicle and place on safety stands. Place a floor jack under center of axle housing. Remove rear wheels. Index mark propeller shaft and companion flange so components can be realigned in original position. Disconnect bolts mounting propeller shaft and carefully guide shaft from vehicle. Separate parking brake linkage at rear coupling and place forward out-of-way. Disconnect brake line rear union and plug opening. Disconnect shock absorbers at lower mount and compress until clear. Lower jack under axle housing and remove nuts and U-bolts securing leaf springs. With axle housing balanced on floor jack, carefully maneuver from vehicle.
Installation - To install axle housing, reverse removal procedure noting the following: Ensure propeller shaft index marks are properly aligned. Be sure U-bolts are not twisted over axle housing and that vehicle weight is on wheels when lower end of shock absorber is tightened.
OVERHAUL
Disassembly
NOTE - Prediassembly inspection of ring gear backlash and gear tooth contact can indicate where possible problems may be oriented. See Gear Tooth Contact at beginning of this section
1) With differential carrier mounted in suitable work stand, index mark side bearing caps and carrier. Remove bearing caps and lift out differential assembly. Remove drive pinion lock nut and pull companion flange off using a gear puller. Remove drive pinion together with rear bearing inner race, spacer and washer. Drive pinion can be freed by tapping front ed of assembly. If necessary, extract oil seal and withdraw front bearing inner race.
2) Using suitable puller (ST300310000) extract pinion. To take out both front and rear bearing outer races, use drift placed on race side surface and tap out. To disassemble differential gear case proceed as follows: Using a suitable puller (ST3305001) remove side bearings. Keep right and left side components separated for reassembly. Lift ring gear bolt lock tabs and remove bolts by loosening in a diagonal sequence. Using a punch, top out pinion gear lock pin and remove pinion gears, side gears and thrust washers. Identify gears and thrust washers for ireinstallation.

Thoroughly clean all disassembled parts and visually inspect for excessive wear. Check all gears for wear and replace when necessary. NOTE - Drive pinion and ring gear are replaced only as a set. Inspect thrust washer surfaces and be sure they are free from surface scratches.
REASSEMBLY
 |
| ADJUSTING PINION HEIGHT |
Drive Pinion Height - Pinion height is adjusted with drive pinion adjusting washer placed behind the drive pinion gear. Variation from the standard size ot the drive gear center is marked on drive pinino gear head. If tolerance is greater than standard size, number is marked in "+", if less than standard size, marking is "-". Install front and rear drive pinion outer races in gear carrier. Fit drive pinion adjusting washers and bearing on suitable dummy shaft. Position dummy shaft in final drive housing without drive pinion adjusting spacer, then pu on front pinion bearing and companion flange. Tighten drive pinion nut to specified preload setting. Fit suitable drive pinion height gauge on final drive housing and measur clearance between end of gauge and surface of dummy shaft as shown in illustration. To calculate thickness of needed drive pinion adjusting washer, use the following formula:
 |
| MEASURING CLEARANCE BETWEEN HEIGHT GAUGE AND DUMMY SHAFT |
T = Thickness of needed shim.
W = Thickness of temporary shim.
N = Clearance between depth gauge and dummy shaft.
H = Figure stamped on drive pinion head.
NOTE - Formula values are expressed in millimeters.
Remove dummy shaft from gear carrier, take out pinion rear bearing from dummy shaft, select correct shims based on calculation and refit pinion rear bearing and drive pinion. Ensure face side of shims are toward back of pinion gear.
Drive Pinion Preload, Non-Collapsible Spacer Type - Adjustment of drive pinion preload is accomplished with spacer and washers placed between front and rear inner bearing races. NOTE - Adjustment must be performed without oil seal installed. Proceed with adjustment as follows:
Liberally lubricate pinion bearings and install in the following order; drive pinion, spacer, washer, front inner race, companion flange and flat washer. Tighten nut to specified torque. Rotate pinion by hand so pinion nut is not over tightened. Increase spacer and washer thickness when pinion will no longer turn. Using a suitable pinion bearing preload gauge, determine the correct washer and spacer needed to provide specified epreload. Spacers and washers are available in various sizes. Insert proper spacer and washer and again check preload. If preload is within specifications, remove drive pinion nut and companion flange, then press in a new oil seal. Install companion flange and tighten nut.
Drive Pinion Preload, Collapsible Spacer Type - After obtaining final pinion bearing height, lubricate front bearing and place into carrier. Fit new oil seal in carrier and fill space between seal lips with grease. Slip new collapsible spacer on drive pinion, then lubricate pinion rear bearing. Insert companion flange in oil seal while holding flange tightly against pinion bearing cone. Working from back of carrier, insert drive pinion into the companion flange. Ensure drive pinion threads and mounting nut are dirt free, then holding companion flange, tighten nut. This step will pull drive pinion front bearing cone and flange. When drive pinion is pulled into bearing cone bearing end play will be reduced. With end play still in evidence, companion flange will be felt bottoming on collapsible spacer. Slowly turn nut and continiously check end play to ensure bearing preload does not exceed specifications. When end play is eliminated final preload is being approached. Turn pinion in both direction to set bearing. Adjust bearing preload to specifications using suitable gauge (ST31275000).
NOTE - Never try to decrease bearing preload by backing off pinion nut; always replace collapsible spacer.
 |
| CALCULATING SIDE BEARING SHIM THICKNESS |
Left Side: T = (A-C + D-H') x .01 + .2 + E
Right Side T = (B-D + H') x .01 + .2 + F
T = Shim thickness.
B = Figure stamped on right side bearing.
C & D = Figure stamped on differential case (+ or 0 number).
E & F = Deviation from standard bearing thickness.
H' = Figure stamped on ring gear.
 |
| MEASURING DISTANCE BETWEEN BEARING CAPS |
2) Side bearing thickness is measured using a suitable press (ST3250S0000) and applying approximately 5.5 lbs. (2.5 kg). Measure thickness in at least three locations.
3) Fit side bearing shim of differential case and press in both side bearing inner races. Place differential case assembly into gear carrier, then install bearing cap on carrier.
4) As a second check, measure distance between bearing caps using a micrometer (see illustration).. Specification obtained should be as indicated in table. Correct any deviation with the proper shim.
 |
| MEASURING RING GEAR BACKLASH |
6) Check side bearing preload by measuring amount of rotating torque needed to turn compoanion flange (see illustration). Check gear tooth contact pattern and correct any problem. NOTE - See Gear Tooth Contact Pattern at beginning of this section.


 |
| MEASURING DRIVE PINION PRELOAD |


Wednesday, March 28, 2012
Datsun 1968-76 Drive Axles Repair Manual
1968-74 DATSUN INTEGRAL HOUSING (I.R.S)
- 510 (1968-72)
- 610 Sedan and Hardtop (1973-74)
- 240Z (1970-73)
- 260Z (1974)
DESCRIPTION
The axle assembly is the hypoid gear type with integral carrier housing. The pinion bearing preload adjustment is made with a spacer and washer between the front and rear bearing cones. The differential side bearing preload and the pinion depth adjustment are made by shims. Driving power is transmitted to the rear axle by ball spline type driveshaft with universal joints at both ends.
AXLE RATIO AND IDENTIFICATION
All Datsun models with Independent Rear Suspension (I.R.S.), use one basic type rear axle assembly. Any differences in Removal and Installation or Overhaul procedures will be noted where they occur. To determine axle ratio, divide number of ring gear teeth by number of pinion teeth.
REMOVAL AND INSTALLATION
Axle Shaft and Bearings
Removal - Raise and support vehicle and remove wheel and brake drum. Disconnect driveshaft from axle outer flange. Remove wheel bearing lock nut while holding axle shaft outer flange stationary. Using suitable axle stand (ST07640000) and slide hammer, remove axle shaft. Remove wheel bearing spacer, companion flange and bearing washer, then remove inner wheel bearing and oil seal. Remove grease catcher, then press or pull outer wheel bearing from axle shaft. NOTE - Do not reuse old outer wheel bearing.
 |
| REAR AXLE ASSEMBLY (MODEL 610 SHOWN) |
Installation - To install, reverse removal procedure and note the following: Clean and inspect all parts for wear or damage and replace as necessary. Grease wheel bearings and housing before installation. When installing bearings ensure outer bearing is installed with seal towards wheel and that inner bearing is installed with seal facing differential. A mark "A", "B" or "C" is stamped on axle housing. Ensure that bearing spacer with same mark is installed. Tighten all bolts and nuts and adjust wheel bearings.
Wheel Bearing Adjustment - After tightening wheel bearing lock nut to specification, check that axle shaft end play is .006" (.15 mm) or less. Check that turning torque of axle shaft is less than 1.8 lbs (.8 kg) at hub bolt. If either adjustment is not to specification, disassemble axle shaft assembly and replace bearing spacer.
DRIVE SHAFTS
Removal and Installation - Raise and support rear of vehicle on safety stands. Disconnect drive shaft from axle shaft companion flange. Remove differential side yoke attaching bolt and lift out side yoke and drive shaft as an assembly. To install, reverse removal procedure and note the following: Exercese care when installing assembly to prevent damage to side yoke and oil seal. Tighten all bolts to specifications.
PINION FLANGE AND OIL SEAL
Removal - Drain gear oil from differential, then raise and support rear of vehicle. Disconnect propeller shaft from pinion flange, then if necessary remove muffler and disconnect parking brake cable. On 240Z and 260Z models remove rear stabilizer from vehicle. On all models, remove pinion nut, while holding pinion flange stationary. Using a suitable puller remove pinion flange. Remove oil seal using suitable puller (ST33290001).
Installation - To install, reverse remove procedure and note the following: Apply suitable grease between seal lips before installation. Tighten pinion nut to specifications and ensure pinion bearing preload is correctly adjusted. Fill differential to proper level gear oil.
AXLE ASSEMBLY
Removal - Raise and support rear of vehicle. On all models except 240Z and 260Z disconnect parking brake cable from turnbuckle. On 240Z and 260Z models, remove main muffler. On all models, disconnect propeller shaft from axle assembly. On 240Z and 260Z models, loosen front side transverse link inner bolts. On all models, remove axle drive shafts. Support axle assembly on a jack, then remove nuts on both ends of axle assembly rear mounting member. Remove axle assembly front mount attaching bolts, lower assembly on jack and remove from vehicle. NOTE -On all models except 240Z and 260Z, support suspension member tor prevent damage to insulators.
Installation - To install, reverse removal procedure and note the following: Install same size mounting spacer between axle assembly and front mount. Tighten all nuts and bolts to specifications and fill assembly to correct level with gear oil.
DRIVE SHAFT OVERHAUL
DISASSEMBLY
 |
| DRIVE SHAFT ASSEMBLY |
NOTE - Drive shaft should be disassembled only to lubricate ball spline.
Remove universal joint from differential end of drive shaft. Remove snap ring from sleeve yoke plug and remove plug. Compress drive shaft and remove snap ring from stopper, then remove stopper. Disconnect boot and separate drive shaft carefully as not to loose balls and spacers.
DRIVE SHAFT ASSEMBLY
INSPECTION
Check rubber boot and oil seeds for damage and replace as necessary. Inspect drive shaft for straightness, crack, damage and distortion and replace drive shaft if necessary. Check all other drive shaft assembly if any faulty part is found. Check drive shaft play as shown in illustration and replace complete assembly if play exceeds .004" (1 mm). NOTE - Measurement should be taken with drive shaft fully compressed.
REASSEMBLY
To reassemble, reverse disassembly procedure and note the follwing: Align yokes and ensure steel balls and spacers are installed in correct order. Adjust axial play of universal joint to within .0008" (.02 mm) by selecting proper size snap ring. NOTE - Snap rings are available in four sizes: .0587" (1.49 mm); .0598" (1.52 mm); ..0610" (1.55 mm); .0622" (1.58 mm). Apply grease to ball grooves and oil grooves.
AXLE ASSEMBLY AND OVERHAUL
1) Mount axle assembly on suitable holding fixture. Remove rear mounting member and axle assembly cover plate. Using suitable puller, remove side reatainers and shims (610), or side flange, bearing cap screws, caps and shims (280Z) NOTE - Mark retainers or bearing caps and shims for reassembly. Left and right sides are not interchangeable. If side bearings on the 610 model are to be replaced, remove bearing outer race from side retainer using a suitable puller.
2) Hold pinion flange stationary and remove pinion nut, then using suitable puller, remove pinion flange. Press drive pinion from carrier and remove rear bearing inner race, bearing spacer and adjusting washers. Remove oil seal. Remove pilot bearing together with pilot bearing spacer and front bearing inner race. Press rear bearing inner race from drive pinion. Using a drift, remove front and rear bearing outer races.
3) To disassemble differential case, use suitable puller and remove side bearings. NOTE - Keep left and right side bearings separate, they are not interchangeable. Remove ring gear by unfolding lock strap and loosening bolts. Punch off pinion shaft lock pin from ring gear side, then remove pinion shaft, pinion gears, side gears and thrust washers. NOTE - Mark gears and thrust washers for instaallation in their original position. Thoroughly clean and inspect all parts for wear or damage and repair or replace as necessary.
Differential Case Assembly - 1) Assemble pinion gears, side gears and thrust washers in original position in differential case. Fit pinion shaft to differential case so that it aligns with lock pin holes. Adjust side gear-to-pinion gear backlash or adjust clearance between rear face of side gear and thrust washer. Install pinion shaft lock pin and lock in place with punch.
2) Apply gear oil to gear tooth surface and thrust surfaces and ensure gears rotate smoothly. Install ring gears on differential case and install bolts and new lock washers. NOTE -Tighten ring gear bolts diagonally while tapping around bolt heads with a hammer.
REASSEMBLY
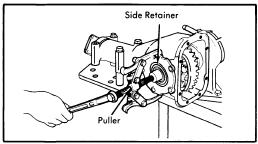 |
| FIG. 4 REMOVING SIDE RETAINER (610 MODEL) |
AXLE ASSEMBLY AND OVERHAUL
1) Mount axle assembly on suitable holding fixture. Remove rear mounting member and axle assembly cover plate. Using suitable puller, remove side reatainers and shims (610), or side flange, bearing cap screws, caps and shims (280Z) NOTE - Mark retainers or bearing caps and shims for reassembly. Left and right sides are not interchangeable. If side bearings on the 610 model are to be replaced, remove bearing outer race from side retainer using a suitable puller.
 |
| FIG. 5 REMOVING PINION GEAR BEARING INNER RACE |
3) To disassemble differential case, use suitable puller and remove side bearings. NOTE - Keep left and right side bearings separate, they are not interchangeable. Remove ring gear by unfolding lock strap and loosening bolts. Punch off pinion shaft lock pin from ring gear side, then remove pinion shaft, pinion gears, side gears and thrust washers. NOTE - Mark gears and thrust washers for instaallation in their original position. Thoroughly clean and inspect all parts for wear or damage and repair or replace as necessary.
REASSEMBLY AND ADJUSTMENT
 |
| FIG. 7 MEASURING SIDE BEARING WIDTH |
 |
| FIG. 6 MEASURING SIDE GEAR CLEARANCE |
2) Apply gear oil to gear tooth surface and thrust surfaces and ensure gears rotate smoothly. Install ring gears on differential case and install bolts and new lock washers. NOTE -Tighten ring gear bolts diagonally while tapping around bolt heads with a hammer.
 |
| MEASURING DRIVE SHAFT PLAY |
3) When replacing side bearings, measure bearing width with a .787" (20 mm) gauge and 5.5 lb (2.5 kg) weight block. Bearing width should be slightly smaller than gauge. Press fit side bearing inner race on differential case and side bearing outer race into side retainers. Install new oil seal on side retainer and apply grease to cavity between seal lips.
Drive Pinion Preload - 1) NOTE - Perform adjustment without pinion shaft oil seal installed. Press fit and rear bearing outer races into gear carrier. Insert suitable dummy shaft spacer (ST31851000), pinion height adjusting spacer and rear bearing inner race into suitable dummy shaft (ST31212000).
2) Fit drive pinion bearing spacer, washer, front bearing inner race, suitable dummy shaft collar (ST31214000) and pinion flange on dummy shaft and tighten drive pinion nut to specified torque.
 |
| ADJUSTING DRIVE PINION PRELOAD |
3) Measure pinion bearing preload using suitable preload gauge (ST31275000) and select washer and spacer that will provide specified preload. NOTE - Preload of old bearing is the same as that of a new bearing. Pinion bearing adjusting washers are available in thicknesses of .0906-.1024" (2.3-2.6 mm). Pinion bearing adjusting spacers are available in lengths at 2.2126-2.22520" (56.2-57.2 mm) on 610 models and 2.0551-2.0945" (52.2-53.2 mm) on all other models.
DRIVE PINION HEIGHT - 1) Install suitable height gauge (ST3121000) on gear carrier with dummy shaft mounted. Measure clearance between tip end of height gauge and end surface of dummy shaft. Thickness of drive pinion height adjusting washer can be obtained by the following formula.
 |
| MEASURING DRIVE PINION HEIGHT |
T=W + N - (H - D' - S) x.01 - .2
NOTE - Formula values are give in Millimeters
T = Thickness of adjusting washer needed.
W = Thickness of washer temporarily installed.
N = Clearance between gauge and dummy shaft.
D' = Figure marked on dummy shaft
S = Figure marked on height gauge
NOTE - If values signifying H, D, and S are not given, regard them as zero.
2) Fit correct pinion adjusting washer in drive pinion and press fit rear bearing inner race. Lubricate pinion front and rear bearings, then install drive pinion in carrier along with drive pinion bearing spacer and washer, front bearing race, front bearing pilot spacer, pilot bearing and oil seal. Install pinion flange and tighten pinion nut to specifications
Side Bearing Preload - 1) Required thickness of left and right side retainer shims can be obtained by the following formulas
 |
| SIDE BEARING PRELOAD FORMULA VALUES |
T1 = (A + C + G1 - D) X .01 + .76 - E
T2 = (B + D+ G2) X .01 + .76 - F
NOTE - Formula values are given in millimeters
T1 = Required thickness of left side retainer shim.
T2 = Required thickness of right side retainer shim.
A & B = Figure marked on gear carrier.
C & D = Figure marked on differential case.
E & F = Difference in width of left or right bearing.
G1 and G2 = Figure marked on left or right retainers.
NOTE - If values signifying A,B,C,D,G1 and G2 are not given, regard them as zero.
2) Install differential case assembly in gear carrier in reverse order of disassembly. Fit correct shims and "O" ring seal in both side retainers and install retainers in carrier with arrow pointing as shown in illustration.
 |
| SIDE BEARING PRELOAD IDENTIFICATION MARKS |
 |
| INSTALLING SIDE RETAINER |
3) Using dial indicator, remove ring gear-to-drive pinion backlash and adjust if necessary. Check side bearing preload, and adjust if necessary by adding or removing side retainer shims. NOTE - If side bearing preload is readjusted, ring gear-to-drive pinion backlash must be checked and adjusted. If necessary
Final Inspection and Assembly - After all adjustments are to specifications, make tooth contact pattern test and make any necessary correction. See Gear Tooth Contact Pattern of beginning of this section. Install rear cover and tighten nuts to specifications. Refill axle assembly to correct level with gear oil.
 |
| MEASURING RING GEAR BACKLASH |

Friday, March 23, 2012
Arrow/Colt 1976-77 Drive Axles Repair Manual
DESCRIPTION
Rear axle is of the banjo type, utilizing the removable carrier style differential. Light weight construction joins split tubular housings for each side with center covers welded to axle housing. Final drive is of the hypoid style. Axle shafts are semi-floating type supported with bearings at their respective ends in axle housing. Bearings are fitted to axles with pressure type bearing retainers. Pinion bearing preload side bearing preload, and pinion depth adjustment are made with shims while differential side gears are adjusted with spacers
REMOVAL AND INSTALLATION
Axle Shafts and Bearings
 |
| FIG. 1 MEASURING AXLE SHAFT DEFLECTION |
2) To remove axle bearing proceed as follows: Grind down bearing retainer at one point until retainer thickness is .04-.06" (1.0-1.5 mm), then chisel ground portion and remove retainer. Using suitable bearing puller or press (CT-1120) remove bearing from axle.
3) Using a dial indicator, inspect axle shaft deflection in three spots (see illustration). Replace axle shaft if specifications are exceeded.
4) Rear axle bearing should be replaced when bearing noise is detected, when bearing axial free play exceeds .014-.016" (.36-.41 mm) or if bearing radial free play exceeds .001-.002" (.03-.04 mm) at approximately 11 lbs. (5.0 kg) measuring force.
5) Inspect wheel hub bolts for tightness and bearing outer retainer for deformation ,replace defective parts as nessary.
Installation - 1) Fit outer bearing retainer flat side against shaft splined end, then install bearing and inner bearing retainer. Seat bearing retainer with smaller chamfered side directed to the bearing. NOTE -Ensure bearing is completely seated.
2) Lightly coat lips of oil seal and using suitable oil seal installer (DT-1007B & CT-1008) fit axle shaft oil seal in rear axle housing.
3) Using packings and shims in proper sequence, set clearance between bearing and outer bearing retainer to .00-.01" (.0-.25 mm).
4) Carefully insert axle shaft assembly into axle housing using care not to damage seal. Slightly turn shaft until splines line up with differential side gears. Align packing oil holes with outer bearing retainer and tighten bearing retainer to axle housing flange. Connect brake line to wheel cylinder and bleed air from system.
DIFFERENTIAL CARRIER
Removal - Drain oil from rear axle differential housing, then disconnect propeller shaft. Pull out both rear axle shafts approximately 2 1/3". Remove differential gear housing mounting nuts and withdraw the differential gear carrier. It may be necessary to top outside of housing to break gear carrier loose.
Installation - Lightly coat each bearing and gear with oil. Apply sealing compound on packing and axle housing seat, then assemble gear carrier to housing with nuts and tighten. Fill differential gear housing with .96 quart of suitable multi-purpose gear oil (API GL-5).
Differential Gear Assembly - 1) Remove bearing carrier cap and lever gear case assembly from housing. Using suitable bearing puller tool (C-293-P & C293-39) pull differential side bearing. Keep right and left bearings and shims in sequence for reassembly
2) Remove ring gear lock plate tabs and loosen bolts in diagonal sequence, then remove ring gear. Drive out pinion shaft lock pin from ring gear back side using a punch, pull out pinion shaft and pinion. Pinion side gears and spacers are now accessible. Note placement of side gear and spacers and ensure they are reassembled in same position.
Drive Pinion Disassembly - 1) Hold end yoke with suitable tool (C-3281) and remove lock nut, then remove end yoke. Using a wheel puller, force out drive pinion with adjusting shim, rear inner bearing race, spacer and preload adjusting shim.
2) With suitable bearing puller (C-293-P & C-293-39) remove rear bearing inner race and at same time, pull of dive pinion adjusting shim. Using suitable drift, remove front drive pinion bearing outer race and oil seal. Repeat some procedure to remove bearing outer race.
INSPECTION
Check differential gears for correct tooth contact and replace gears if wear is excessive. Inspect bearing faces for roughness or score marks and replace, if necessary, bearing assembly. Ensure splines of side gears and rear axle shafts fit correctly. Check clearance between pinion gears and pinion shaft, if wear is excessive, replace components.
NOTE - To check gear tooth contact using pain impression method, refer to beginning of this section.
REASSEMBLY AND AJDUSTMENT
Case Assembly - 1) Install thrust washers (spacers) behind side gears in their original position and assemble pinion and side gears in differential. Insert both pinion gears with pinion washers attached, so they mesh with side gears. It may be necessary to slightly rotate pinions to achieve desired meshing. Insert drive pinion shaft.
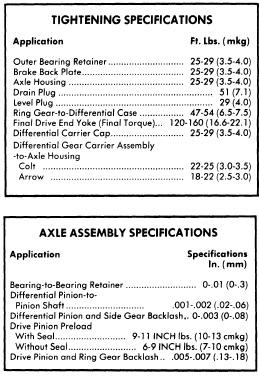
2) Check pinion and side gear backlash as shown in illustration. If backlash is beyond 0-.003" (0-.08mm) adjust by selecting a side gear thrust washer (spacer) of correct size. If backlash is to be adjusted, ensure right and left sides are equally shimmed.
3) Thoroughly clean all dirt from ring gear mounting surface of differential case. Install bolts and lock washers. Tighten bolts alternately in a diagonal sequence and bend over lock tabs. Ensure lock washers are in contact with case rib after final torque is performed.
Drive Pinion - Using a suitable drift and hammer or a press, seat front and rear bearing outer races into gear carrier ensuring that outer races do not cock. Ensure bearing races are completely seated before proceeding. Install shim between drive pinion and rear bearing. Using suitable bearing installer (CT-1075) press bearing onto drive pinion shaft. If drive pinion and bearings are scheduled to be reused, shims should be replaced with new ones of same thickness. In instances where the gear set is to be replaced, install new shims that are the same thickness as the used shims on drive pinion NOTE - When determining the desired thickness of shim pack, amount of compression the desired thickness of shim pack, amount of compression (sinkage) of shim pack and wear of the beating (where old bearing is reused) must be taken into consideration.
Drive Pinion Depth - Install drive pinion spacer, front bearing, washer, end yoke and washer in order of removal. Fit pinion shaft retaining nut and slowly tighten nut, continously checking, until pinion bearing preload is 6-9 INCH lbs (7-10 cmkg) with oil seal not installed. Place suitable cylinder gauge on inside bearing pedestals of gear carrier housing. Place a block gauge on top end of drive pinion and slip a feeler gauge between the two gauges should be .0118" (.300 mm). This is the standard height and any deviation from this height will be marked on the head of the pinion shaft and side of ring gear. To calculate the correct pinion height, add or subtract the variation value from the standard height.
NOTE - Stamped values are in hundredth millimeters. Add or subtract the correct amount of shims an necessary.
Pinion Bearing Preload - The adjustment must be performed after the setting of the drive pinion depth. Remove end yoke and insert the bearing preload adjusting shim between pinion spacer and bearing, then tighten end yoke to 9-11 INCH lbs. (10-13 cmkg). In addition to the preload adjusting shims there are spacers available to provide proper adjustment. After finishing adjustment of drive pinion bearing preload remove the end yoke and apply a thin coat of grease to outer surface of oil seal, then drive seal into position in gear carrier. After greasing oil seal lip, insert end yoke and tighten nut.
Side Bearing Preload - Fit each side into differential case leaving shims out; use suitable tool (CT-1102) for this procedure. Ensure side bearings are completely seated before proceeding. Install differential case assembly on gear carrier, then calculate the clearance between side bearing outer race and gear carrier as shown in illustration. After obtaining clearance add .002" (.05 mm) preload figure to each side. Insert shims equally on both sides. Align gear carrier end bearing cap index marks, then tighten cap retaining bolts.
Ring Gear Deflection - Attach a dial indicator to back side of ring gear and measure deflection. If ring gear has excessive deflection, correct position of the assembly in relation to differential case and again perform measurement. Replace ring gear or differential case as necessary.
Drive Pinion Depth - Measure backlash of drive pinion is at least four different spots on ring gear with drive pinion securely fixed in final position. Set up a dial indicator on ring gear teeth edges. If measured backlash is greater than .005-.007" (.13-.18 mm), shift shims from ring gear side to the back of the ring gear to obtain pro[er backlash. If the measure value is less than standard value, reverse the moving of shims as stated above. Side bearing shims are available in various thicknesses.
NOTE - Check gear tooth contact patter using point impression method described at beginning of this section.
Final Inspection and Assembly - Lightly coat each gear and bearing before and during reassembly with gear oil. After installing each component, ensure all rotating parts are free to move smoothly. Install differential gear assembly to axle housing after applying sealing agent and tighten gear carrier mounting nuts in diagonal sequence.
4) Rear axle bearing should be replaced when bearing noise is detected, when bearing axial free play exceeds .014-.016" (.36-.41 mm) or if bearing radial free play exceeds .001-.002" (.03-.04 mm) at approximately 11 lbs. (5.0 kg) measuring force.
5) Inspect wheel hub bolts for tightness and bearing outer retainer for deformation ,replace defective parts as nessary.
Installation - 1) Fit outer bearing retainer flat side against shaft splined end, then install bearing and inner bearing retainer. Seat bearing retainer with smaller chamfered side directed to the bearing. NOTE -Ensure bearing is completely seated.
 |
| FIG. 2 EXPLODED VIEW OF AXLE SHAFT ASSEMBLY |
3) Using packings and shims in proper sequence, set clearance between bearing and outer bearing retainer to .00-.01" (.0-.25 mm).
4) Carefully insert axle shaft assembly into axle housing using care not to damage seal. Slightly turn shaft until splines line up with differential side gears. Align packing oil holes with outer bearing retainer and tighten bearing retainer to axle housing flange. Connect brake line to wheel cylinder and bleed air from system.
DIFFERENTIAL CARRIER
 |
| FIG. 3 REMOVING DIFFERENTIAL GEAR HOUSING |
Installation - Lightly coat each bearing and gear with oil. Apply sealing compound on packing and axle housing seat, then assemble gear carrier to housing with nuts and tighten. Fill differential gear housing with .96 quart of suitable multi-purpose gear oil (API GL-5).
OVERHAUL
Disassembly |
| FIG. 4 REMOVING DIFFERENTIAL SIDE BEARINGS |
2) Remove ring gear lock plate tabs and loosen bolts in diagonal sequence, then remove ring gear. Drive out pinion shaft lock pin from ring gear back side using a punch, pull out pinion shaft and pinion. Pinion side gears and spacers are now accessible. Note placement of side gear and spacers and ensure they are reassembled in same position.
Drive Pinion Disassembly - 1) Hold end yoke with suitable tool (C-3281) and remove lock nut, then remove end yoke. Using a wheel puller, force out drive pinion with adjusting shim, rear inner bearing race, spacer and preload adjusting shim.
 |
| FIG. 6 REMOVING DRIVE PINION FRONT BEARING OUTER RACE |
INSPECTION
Check differential gears for correct tooth contact and replace gears if wear is excessive. Inspect bearing faces for roughness or score marks and replace, if necessary, bearing assembly. Ensure splines of side gears and rear axle shafts fit correctly. Check clearance between pinion gears and pinion shaft, if wear is excessive, replace components.
NOTE - To check gear tooth contact using pain impression method, refer to beginning of this section.
 |
| FIG. 7 EXPLODED VIEW OF COLT SEPARATE HOUSING REAR AXLE ASSEMBLY |
REASSEMBLY AND AJDUSTMENT
 |
| FIG. 8 CHECKING DIFFERENTIAL PINION AND SIDE GEAR BACKLASH |
2) Check pinion and side gear backlash as shown in illustration. If backlash is beyond 0-.003" (0-.08mm) adjust by selecting a side gear thrust washer (spacer) of correct size. If backlash is to be adjusted, ensure right and left sides are equally shimmed.
3) Thoroughly clean all dirt from ring gear mounting surface of differential case. Install bolts and lock washers. Tighten bolts alternately in a diagonal sequence and bend over lock tabs. Ensure lock washers are in contact with case rib after final torque is performed.
Drive Pinion - Using a suitable drift and hammer or a press, seat front and rear bearing outer races into gear carrier ensuring that outer races do not cock. Ensure bearing races are completely seated before proceeding. Install shim between drive pinion and rear bearing. Using suitable bearing installer (CT-1075) press bearing onto drive pinion shaft. If drive pinion and bearings are scheduled to be reused, shims should be replaced with new ones of same thickness. In instances where the gear set is to be replaced, install new shims that are the same thickness as the used shims on drive pinion NOTE - When determining the desired thickness of shim pack, amount of compression the desired thickness of shim pack, amount of compression (sinkage) of shim pack and wear of the beating (where old bearing is reused) must be taken into consideration.
Drive Pinion Depth - Install drive pinion spacer, front bearing, washer, end yoke and washer in order of removal. Fit pinion shaft retaining nut and slowly tighten nut, continously checking, until pinion bearing preload is 6-9 INCH lbs (7-10 cmkg) with oil seal not installed. Place suitable cylinder gauge on inside bearing pedestals of gear carrier housing. Place a block gauge on top end of drive pinion and slip a feeler gauge between the two gauges should be .0118" (.300 mm). This is the standard height and any deviation from this height will be marked on the head of the pinion shaft and side of ring gear. To calculate the correct pinion height, add or subtract the variation value from the standard height.
NOTE - Stamped values are in hundredth millimeters. Add or subtract the correct amount of shims an necessary.
Pinion Bearing Preload - The adjustment must be performed after the setting of the drive pinion depth. Remove end yoke and insert the bearing preload adjusting shim between pinion spacer and bearing, then tighten end yoke to 9-11 INCH lbs. (10-13 cmkg). In addition to the preload adjusting shims there are spacers available to provide proper adjustment. After finishing adjustment of drive pinion bearing preload remove the end yoke and apply a thin coat of grease to outer surface of oil seal, then drive seal into position in gear carrier. After greasing oil seal lip, insert end yoke and tighten nut.
Side Bearing Preload - Fit each side into differential case leaving shims out; use suitable tool (CT-1102) for this procedure. Ensure side bearings are completely seated before proceeding. Install differential case assembly on gear carrier, then calculate the clearance between side bearing outer race and gear carrier as shown in illustration. After obtaining clearance add .002" (.05 mm) preload figure to each side. Insert shims equally on both sides. Align gear carrier end bearing cap index marks, then tighten cap retaining bolts.
 |
| FIG. 9 MEASURING CLEARANCE BETWEEN SIDE BEARING AND GEAR CARRIER |
Drive Pinion Depth - Measure backlash of drive pinion is at least four different spots on ring gear with drive pinion securely fixed in final position. Set up a dial indicator on ring gear teeth edges. If measured backlash is greater than .005-.007" (.13-.18 mm), shift shims from ring gear side to the back of the ring gear to obtain pro[er backlash. If the measure value is less than standard value, reverse the moving of shims as stated above. Side bearing shims are available in various thicknesses.
NOTE - Check gear tooth contact patter using point impression method described at beginning of this section.
Final Inspection and Assembly - Lightly coat each gear and bearing before and during reassembly with gear oil. After installing each component, ensure all rotating parts are free to move smoothly. Install differential gear assembly to axle housing after applying sealing agent and tighten gear carrier mounting nuts in diagonal sequence.

Thursday, March 22, 2012
Capri II 1976-77 Drive Axles 2 Repair Manual
CAPRI II
DESCRIPTION
An integral type housing, hypoid design, with centerline of pinion set below centerline of ring gear. Semi-floating zxle shafts are retained in housing by ball bearings and a bearing retainer at axle housing by ball bearings and a bearing retainer at axle housing outer ends. All adjustments are performed using selective fit shims and gaskets.
REMOVAL AND INSTALLATION
Axle Shafts and Bearings
1) Remove brake drum retainers and remove brake drum. Remove bolts securing bearing retainer plate to axle housing. These bolts are accessible through holes in axle shaft flange. Pull axle shaft and bearing assembly out of axle housing.
2) Loosen inner retainer ring by nicking it deeply with a cold chisel in several places. It will then slide of easily. Press bearing and seal assembly from axle shaft using arbor press and suitable tool to hold and support bearing.
3) To install, inspect housing and axle shaft and lightly coat wheel bearing base with axle lubricant. Place bearing retainer plate on axle shaft and press new bearing wheel bearing on shaft using suitable tool. NOTE - Do not attempt to press on both bearing and inner retainer at the same time.
4) Using suitable bearing installation tool, press bearing inner retainer ring on shaft until retainer seats firmly against bearing. Insert axle housing and engage splines. Tap shaft into position. Install bolts securing bearing retainer plate and install brake drum and retainers.
REAR AXLE ASSEMBLY
1) Raise vehicle and remove wheels. Mark propeller shaft for proper alignment and disconnect from drive pinion flange. Release pakring brake, then remove locknut and adjusting nut from handbrake cable and disconnect cable from relay lever. Disconnect brake line from brake hose.
2) Raise and support center of rear axle and disconnect shock absorbers from axle. Remove rear axle support. Remove two stabilizer bar retaining clamps from rear axle housing. Remove rear spring "U" bolt nuts and detach bolts and plates. Lift axle assembly and remove from vehicle.
3) To install, lift rear axle assembly into position on springs, being sure that it is correctly located over spring pilot bolts. Align and loosely fit propeller shaft to drive pinion flange. Fit "U" bolts over axle, slide on lower plates, install new locknuts and tighten.
4) Using a suitable tool, hold rear stabilizer bar onto mounting pads on axle housing and install retaining clamps. Insert retaining clamp bolts, check for binding, and tighten. Raise center of rear axle and install shock absorbers. Remove axle support.
5) Reconnect brake line to brake hose and handbrake cable to relay lever on rear axle housing. Adjust nut until relay lever is just clear of stop, tighten locknut. Tighten driveshaft-to-pinion flange bolts and bleed rear brake system. Fill rear axle housing with lubricant, mount rear wheel and lower vehicle.
DIFFERENTIAL CASE
Disassembly - 1) Raise vehicle and remove wheels and axle shaft assemblies. Mark propeller shaft for correct realignment and disconnect from pinion flange. Remove ten cover attaching bolts, cover and gasket and pinion drain rear axle oil. Discard gasket and thoroughly clean cover.
2) Remove differential housing caps and mark caps for correct repositioning. Lift differential out of axle housing using two pry bars. Remove tapered roller bearing from each side of differential assembly using a suitable puller. Remove adjusting shims from differential housing. Remove ring gear attaching bolts and ring gear from differential assembly.
3) Using a suitable drift, remove lock pin securing differential pinion shaft in case and remove pinion gears, side gears and adjusting shims. Using an INCH pound torque wrench on drive pinion retaining nut, note torque required to turn drive pinion gear. Remove torque wrench, hold pinion flange and remove drive pinion retaining nut. Remove pinion flange using a suitable puller, then remove pinion from axle housing. Remove collapsible spacer from drive pinion. Remove large bearing from drive pinion using press and suitable fixtures. Remove outer pinion bearing and seal from axle housing using a suitable drive. Remove bearing races from axle housing using a drift.
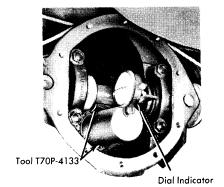 |
| FIG. 1 CHECKING DRIVE PINION DEPTH |
2) Install dummy pinion (part of special tool) into axle housing with pinion bearings but no shims. Lightly lubricate bearings and tighten tool until correct pinion bearing pre-load is obtained. Rotate dummy pinion several times to insure seating of bearings. It is essential that the torque reading be recorded and followed by further adjustment of drive pinion. This torque must also be checked after installation of drive pinion with collapsible spacer.
 |
| FIG. 2 EXPLODED VIEW OF CAPRI II DRIVE AXLE ASSEMBLY |
3) Mound dial indicator as mounting bracket and set to zero on dummy pinion. Slowly rotate dial indicator over cross bar of tool and read total deflection of pointer. This reading gives the exact thickness of the shims to be used. When pinion is marked "-1" or "-2" this amount must be added to indicator reading. When gear is marked "+1" or "+2" this amount must be subtracted from reading to obtain correct shim thickness. Using a micrometer, select a shim of the determined thickness.
 |
| FIG. 3 MEASURING SIDE GEAR CLEARANCE |
5) Position ring gear on differential case and locate with bolts. Pull ring gear evenly into position with bolts. Remove old bolts and install new bolts and tighten. To determine total play of differential case in axle housing. Press tapered roller bearing onto differential case in axle housing: Press tapered roller bearing onto differential case without shims after first inspecting bearing for damage. Install pressure blocks (part of tool T70P-4136) into axle housing on each side of differential case and install differential case and bearings in axle housing. Install bearing caps (number to number) and tighten attaching bolts. Now, loosen bolts and tighten finger tight.
6) Tighten pressure spindle (tool T70P-4136) to a torque of 43 INCH lbs. Rotate differential several times and recheck torque. Mount dial indicator on rear axle housing so that feeler contacts inner side of ring gear flange and zero indicator. Place pressure spindle into other side of housing and tighten to 43 INCH lbs. Read and note amount of indicator deflection and record as play of differential case in rear axle housing. Loosen pressure spindle, tilt dial indicator to side and remove differential, pressure spindle and pressure blocks.
 |
| FIG. 4 DIFFERENTIAL SET-UP, PRESSURE BLOCK AND SPINDLE INSTALLATION |
8) Slowly tighten nut. Keep checking pinion gear rotating torque (using INCH pound torque wrench) until rotating torque is equal to that noted during disassembly. Tighten an additional 2-4 INCH pounds torque for friction of new oil seal. Pinion nut torque should be to specification when pinion rotating torque is correct. If pinion nut torque is below specification and rotating torque is correct, install new collapsable spacer and repeat procedure.
 |
| FIG. 5 MEASURING RING GEAR BACKLASH |
10) Position dial indicator so that feeler contacts ring gear flange and zero indicator. Insert spind into other side of axle housing and torque to 43 INCH lbs. Read and record indicated deflection on indicator as ring gear back side shim thickness. Remove pressure spindle, differential case and pressure blocks from axle housing.
11) To calculate shim thickness, first take the value of differential case total play obtained in step 6) and add to this value a value for ring and pinion backlash which will give an even number. For example, if total play is .0529" (1.344 mm), add for preload the value .0021" (.056 mm) (preload value selected from specified range) to obtain .055" (1.40 mm). Next, take the value for ring gear back side shim thickness, measured in step 10), and subtract .005" (.13 mm) from this value. For example, if ring gear back side shim thickness is .0025" (.64 mm), subtract .005" (.13 mm) to obtain .020" (.51 mm). Now subtract value just obtained (.020" or .51mm) from total play value obtained above (.055" or 1.40 mm) to obtain ring gear face side shim pack, in this example .035" (.89 mm).

13) Position dial indicator feeler in a vertical position on one ring gear tooth and check that pinion to ring gear backlash is to specifications. If not, differential must be removed and shims adjusted. If backlash is to great, remove shims from ring gear back side and vise versa. Do NOT increase or decrease number of shims, but only interchange between one side and the other.
14) Finally check gear tooth contact pattern and adjust as necessary to obtain correct pattern. Position housing cover and new gasket on axle housing and install and tighten bolts. Attach parking brake operating lever to rear axle housing and connect return spring to bracket on housing. Install rear brake assemblies on axle housing and connect parking brake cable to brake assemblies
Tuesday, March 20, 2012
BMW 1975-76 Drive Axles Split Housing Repair Guide
-Models Covered:
REMOVAL AND INSTALLATION
Raise and support vehicle. Remove wheel, drive shaft, axle flange retaining nut, and using a puller, if required, remove axle flange. Using soft headed mallet, drive axle shaft out of housing. Drive out bearings and seals, then remove spacer sleeve and shim. To install, reverse removal procedure noting the following: Install outer bearing then determine distance between outer races of inner and outer bearings. Measure spacer and shim, then install spacer and a suitable shim that will obtain the specified wheel bearing end play. Pack bearings and new seals with suitable grease, then complete installation procedure.
Remove drive shaft. Hold axle flange using suitable tool (7012) and remove flange retaining bolt. Using suitable puller (7011-2) remove axle flange. Pry out oil seal and if required, remove ball bearing on cover side, using suitable puller. To install, reverse removal procedure after packing bearing and/or filling between sealing lips of seal with grease. Install seal flush with housing or cover bore.
Differential Assembly - Remove differential assembly as previously oulined and mount assembly in suitable holding fixture. Drain oil and mark pinion shaft and companion flange far reassembly reference. Remove inspection hole cover, mount dial indicator in one cover bolt hole and check ring gear backface runout and ring-to-pinion gear backlash. Check gear tooth contact pattern. NOTE - Refer to Rear Axle Gear Tooth Patterns in this section. Remove axle flanges and side cover, then remove differential carrier assembly. Proceed as follows for standard or limited slip differential carrier disassembly.
Drive Pinion Gear - 1) Remove differential carrier as previously described, then check pinion bearing preload using an inch pound torque wrench. Remove pinion flange nut lock ring and using a suitable tool (7012) hold flange and remove nut.
Drive Pinion Bearing Preload - 1) If original ring and pinion gear set is being installed, and gear tooth pattern and pinion bearing preload was satisfactory at time of disassembly, install drive pinion gear using original shim and a new collapsable spacer. If a new gear set is being installed, determine correct size of shim to use in the following manner: Drive pinion gears may be stamped either "+1,2,3, etc" or "-1,2,3 etc". Compare marks on tapered ends of old and new gears. Subtract the two numbers. In relation to original shim, a plus remainder means a thinner shim is required; a minus remainder means a thicker shim is required.
Side-to-Pinion Gear Backlash (Standard Differentials) - Install two pinion gears with shaft and one side gear. Mount dial indicator to carrier so plunger contacts side gear. Force side gear hard against pinion gears, zero indicator, then force side gear hard against case. With proper shim and thrust washer, backlash should be as specified, and preload of all three gears should not exceed specified value. Repeat procedure on opposite side (with second set of pinion on four pinion type), then retain side gears pressed outward against carrier so axle flange retaining bolts can later be installed.
 Clutch Assembly End Play (Type 1 Limited Slip Differential) - Assembly cluch assembly without ring gear or case. Apply 220 psi (15.5 kg/sq. cm) to one end of assembly. Measure from inner surface of flange to top surface of spacer ring. Measure depth of case. If clutch assembly-to-housing end play is not to specification, adjust by using thicker or thinner inner clutch disc.
FIG. 10
MEASURING TYPE 1 CLUTCH
ASSEMBLY INSTALLED HEIGHT WITH PRESSURE APPLIED
Checking Pinion Gear Torque (Limited Slip Differentials) - With differential carrier assembled, install axle flanges in carrier. Clamp one flange in vise and using and INCH pound torque wrench (Type 1), or foot pound torque wrench (Type 2), turn other flange. If rotating torque of side and pinion gears i not to specification, install thicker or thinner case cover-to-clutch assembly thrust washers.
Differential Bearing Preload - Install one shim behind carrier bearing outer cone in side cover. Install bearing cone using suitable tool (6053). Install drive flange bolt, without flange, so it contacts pinion gear shaft. Install carrier in housing and tighten cover retaining bolts. Check preload by turning flange bolt using an INCH pound torque wrench. When cover bolts are torqued to specification, measure gap between cover and housing using a feeler gauge. If preload is lower than specified, shims must be thicker than gap; if preload is higher than specified, shims thickness behind cone must be less than gap between cover and housing. Install required shims under bearing cone in cover. Heat ring gear to 176-212 Degrees Fahrenheit, install ring gear on carrier using locking compound on bolts, and install carrier in housing. Check Ring-to-Drive Pinion Gear Backlash.
Ring-to-Drive Pinion Gear Backlash - With differential bearing preload set, remove inspection hole cover, mount dial indicator in one cover bolt hole, and check ring-to-pinion gear backlash. Check ring gear tooth contact pattern. NOTE - Refer to Axle Gear Tooth Patterns in this section. While maintaining established shim thickness, move shims behind carrier bearing outer cones, from one side to the other as necessary, to obtain proper contact pattern. After setting backlash, complete differential reassembly procedure.

- 3.0 Series
- 530 i Series
DESCRIPTION
Differential has hypoid type ring and pinion gear set, and may have one of two clutch pack type limited slip units. Left side of housing is the housing cover and must be removed to expose carrier assembly. Cover incorporates a ball bearing and oil seal for left axle flange, and a bearing cone for the left differential carrier bearing. Right carrier bearing and seal are incorporated in housing. The pinion gear is supported by roller bearings and preload is maintained by a collapsible spacer
AXLE RATIO AND IDENTIFICATION
Ring and pinion gear set with Klingelnberg tooth design, can be identified by the letter "K" stamped on the head of the pinion gear; Gleason teeth are noted by an "H or F" stamping. To determine axle ratio, divide number of ring gear teeth by number of pinion gear teeth. The number of teeth on ring and pinion, and the code for limited slip differential (S40), is stamped on right side of differential housing.


 |
| FIG. 2 EXPLODED VIEW OF HALF SHAFT CONSTANT VELOCITY JOINT |
DRIVE SHAFTS AND UNIVERSAL JOINTS
Remove drive shaft after removing retaining bolts from axle and half shaft flanges. Remove cover from joint housing and snap ring from end of drive shaft. Remove clamps from boot then press drive shaft from joint. Remove dust boot. To install reverse removal procedure using sealer on boot-to-joint surfaces, and install seal cover after packing joint with suitable grease.
 |
| FIG. 1 EXPLODED VIEW OF TYPE 1 AND TYPE 2 LIMITED SLIP DIFFERENTIALS |
AXLE SHAFTS AND BEARINGS
 |
| FIG. 4 PULLING AXLE DRIVE FLANGE |
AXLE FLANGE, SEAL AND BEARING
 |
| FIG. 5 REMOVING AXLE DRIVE FLANGE BEARING |
NOTE - Differential carrier can be removed from housing with differential assembly installed in vehicle. After removing axle flanges, follow Differential Carrier, Disassembly and Overhaul procedure, int his story.
DIFFERENTIAL ASSEMBLY
Remove propeller shaft and drive shafts, tie drive shafts up out of way. Support differential and remove bolts securing it to front brackets and rear support. Remove differential assembly. To install, reverse removal procedure, insuring rear support stress free when installed.
OVERHAUL
Disassembly
 |
| FIG. 6 CHECKING RING GEAR BACKLASH |
Standard Differential Carrier (Two Pinion Type) - Remove carrier bearings using suitable puller (Rolex LM 503349). Separate ring gear from carrier. Drive out pinion shaft lock pin, remove pinion gears shaft and pinion gears, then remove side gears with shims and thrust washers.
Standard Differential Carrier (Four Pinion Type) - Remove carrier bearings using suitable puller (Rolex LM 503349). Separate carrier halfs and lift out pinion gears with shafts, then remove side gears with shims and thrust washers. Remove ring gear from carrier.
Limited Slip Differential Carrier - Remove carrier bearings using suitable puller (Rolex LM 503349). Remove bolts securing case-to-ring gear flange (Type 1), or cover-to-case (Type 2), invert case and lift case off clutch and gear assembly. Separate ring gear from flange. Remove clutch components. Lift off hub, remove side gear and one set of pinion gears. Repeat procedure for other half of case.
 |
| FIG. 7 CHECKING PINION GEAR PRELOAD |
2) Press pinion gear out, through flange and housing, then remove oil seal and front roller bearing. Using suitable puller set (6053), remove pinion bearing outer cones from housing.
REASSEMBLY AND ADJUSTMENT
Differential Assembly - Reverse disassembly procdure noting the following checks and adjustments.
 |
| FIG. 8 SECTIONAL VIEW OF DRIVE PINION GEAR AND BEARING ASSEMBLY |
2) Remove then reinstall pinion gear, using new shim(s), collapsable spacer, and seal as required. Install companion flange and nut and tighten nut to obtain specified drive pinion bearing preload. NOTE - If preload is exceeded, new collapsible spacer must be installed, and this procedure repeated.
 |
| FIG. 9 CHECKING SIDE-TO-PINION |
FIG. 10
MEASURING TYPE 1 CLUTCH
ASSEMBLY INSTALLED HEIGHT WITH PRESSURE APPLIED
 |
| FIG. 11 MEASURING TYPE 2 CLUTCH ASSEMBLY I |
 |
| FIG. 13 MAKING MEASUREMENT FOR ESTABLISHING SHIM PACK FOR DIFFERENTIAL BEARING PRELOAD |
 |
| FIG. 13 MAKING MEASUREMENT FOR ESTABLISHING SHIM PACK FOR DIFFERENTIAL BEARING PRELOAD |
 |
| FIG. 14 SECTIONAL VIEW SHOWING RING GEAR BACKLASH SHIM LOCATIONS |

Subscribe to:
Posts (Atom)